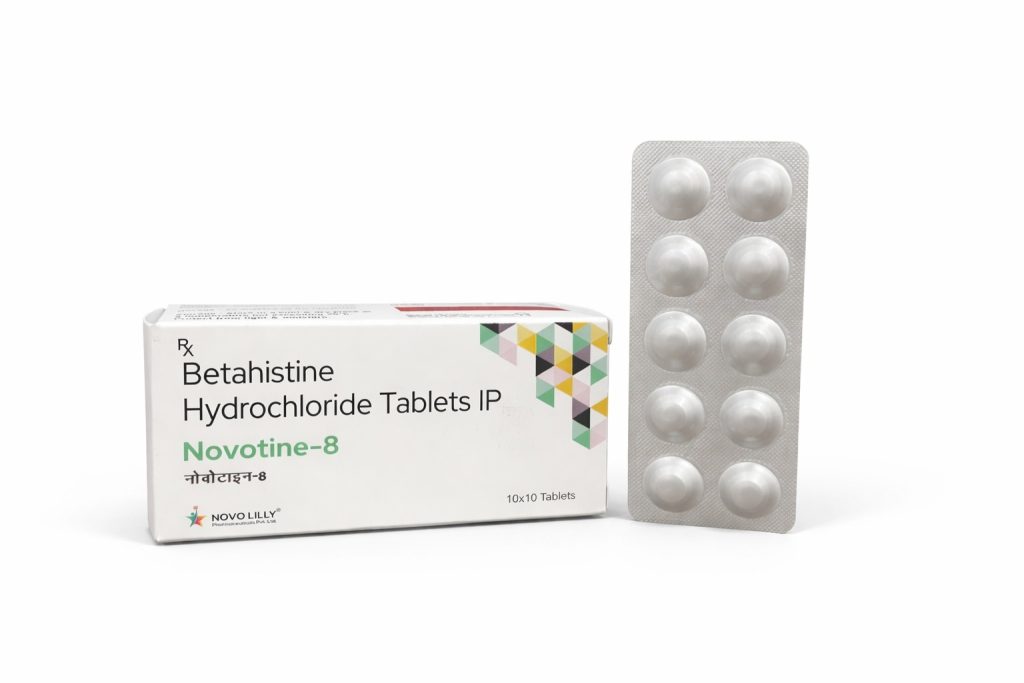
Betahistine 8 MG Tablets Betahistine 8 MG Tablets are a low-dose oral-solid product that contains 8 mg of Betahistine per tablet. Low-dose oral-solid products are challenging to develop because of their need for active-ingredient distribution; the lower quantity of API in the finished product needs to be evenly dispersed throughout the formulation blend. If you're a pharma business looking to broaden your oral-solid dose range with Betahistine 8 MG Tablets, it may be part of a structured PCD Pharma Franchise portfolio.
The excipients suitable for supporting the homogeneous distribution of the active substance within the drug product are selected for the preparation of Betahistina 8 MG Comprimidos. Appropriate diluents, binders, disintegrants, glidants, lubricants, and other approved excipients can be used in the formulation depending on the formulation finalization.
The physical differences between API and excipients such as particle-size distributions and densities may contribute significantly to the blending behavior of a low-strength material. The development of the formulation looks at particle size, bulk density, moisture, flowability and compatibility.
Premixing or geometrical dilution methods should be used where appropriate to achieve good dispersion of the active before the final blend. The aim is to produce a uniform mixture for reproducible tablet compression.
The physical flow of the powder blend impacts directly on manufacturing performance. The formulation for Betahistine 8 MG Tablets should show good flow into the compression tooling whilst exhibiting enough resistance to segregation during manufacturing and transfer.
Sieve selection, blend order, mix time and lubricant addition can all have an impact on the properties of the finished blend. Over handling or inappropriate process conditions can lead to increased segregation potential, a more important consideration for a low dose formulation.
Bulk density, flow properties, moisture content and blend uniformity can be tested during development as well as in-process manufacturing. The results from these tests will determine the operating ranges used in the routine production run.
Once the blend has been prepared, it is compressed into tablets by applying certain time and machine parameters. The compression force, turret speed, feeder parameters, and tooling can all affect the characteristics of the tablet produced.
In-process checks can include weights, thickness, hardness, friability, appearance and other specifications. The tablet weight is of particular importance in that it adds a process indicator for even feeding of the material during compression.
The final tablets should have mechanical resistance sufficient for dedusting, inspection, packaging, transport and storage, while still having a disintegration time and disintegration and dissolution properties within limits specified by the product specification.
Analytical Testing Since the Betahistine 8 MG Tablets product has a relatively low active drug content, testing for Betahistine 8 MG Tablets typically requires at least one of the following: identification, assay, content uniformity, dissolution, related substances, disintegration, or other finished-product parameters.
The analytical techniques used need to be appropriate for the purpose, sensitive enough and validated/qualified as necessary. Sampling techniques should be appropriate to the need, to allow for representative assessment of the batch.
In-process controls can be used to supplement finished-product testing by measuring blend uniformity, tablet weight, compression performance and other key quality attributes. Comprehensive batch records enable traceability and can reveal deviations occurring during manufacturing.
Stability studies are undertaken to determine whether Betahistine 8 MG Tablets: retained within its specified limits throughout its proposed shelf life. As appropriate for the formulation, these include assay, content uniformity (where applicable), dissolution, related substances, appearance, moisture, physical characteristics and packaging integrity.
The packaging should be used in light of the stability profile, which has been recorded, and suitable packaging system such as blister packs/strips or suitable containers system can be assessed for its capacity to protect the tablet from the environmental factor of water.
Compliance with packaging is an essential point the selected composition in addition to ensure various qualities because of the designed material during loading and transportation. The preservation of product qualities, the presence of seals, labels, mark batch expiry date.
Betahistine 8 MG Tablets place more importance on low strength blend uniformity, controlled material flow, sensitive analytics, and uniform compression. This formulation design supports even distribution of the active and physical form across the entire batch of tablets.
This formulation can be a part of a well-structured Oral Tablet range for PCD Pharma Franchise companies manufacturing a diverse PCD Pharma Franchise portfolio. This can also be backed by raw-material specifications, processing parameters, analytical testing, and stability testing.
Reproducible product quality through each step of the process, from API characterization, low strength premixing and compression, through content determination and stability, down to moisture-protection packaging Formulation-specific manufacturing ensures consistent strength and quality of Betahistine 8 MG Tablets through each batch and for the duration of shelf life.
Betahistine 8 MG Tablets formulation, low-strength blend development, manufacturing, quality control, stability and packaging details.