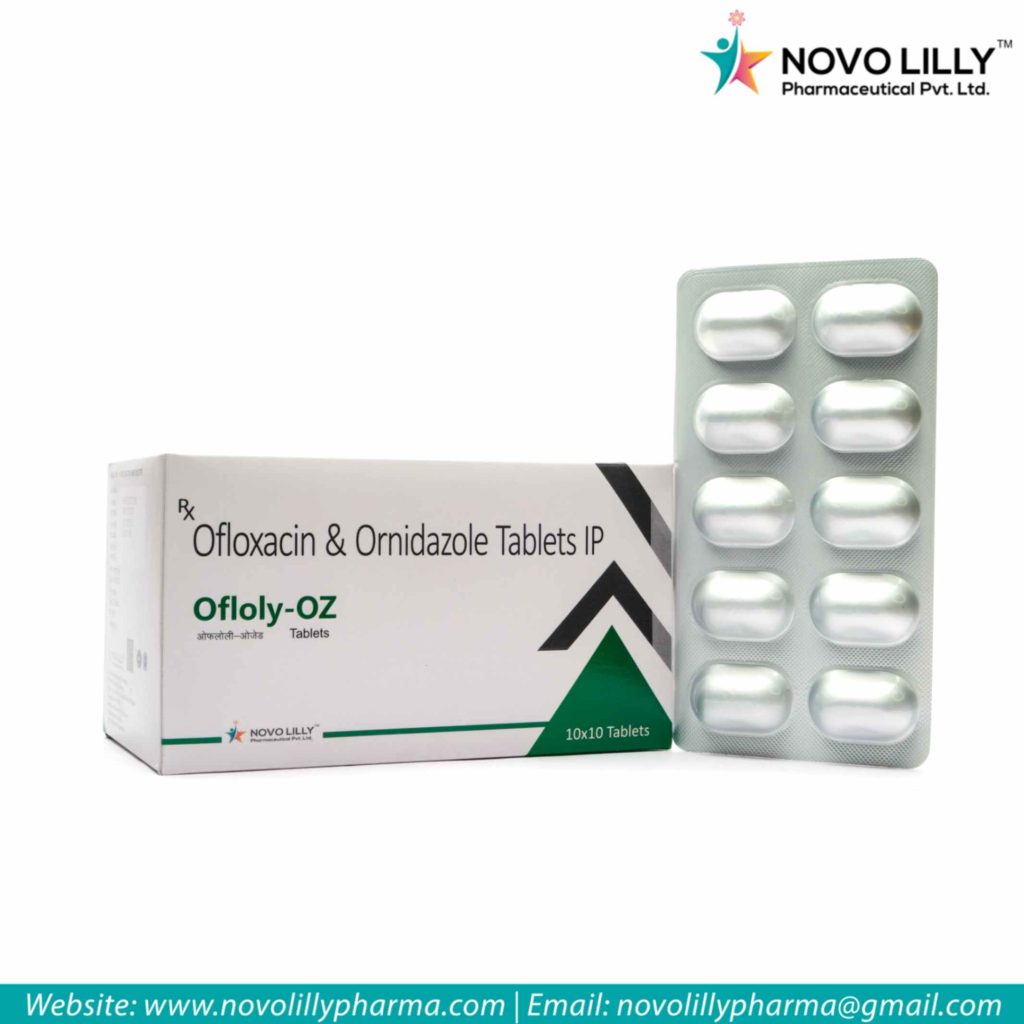
Ofloxacin 200MG + Ornidazole 500MG Tablets have a fixed dose combination of two pharmaceutical ingredients, manufactured as a single tablet. As a formulation with a high total active load, the size of the tablet, the powder density, the compressibility and the spatial distribution of the ingredients are significant in the drug-development process. This formulation of individual pharma companies can be part of a structured PCD Pharma Franchise range with specified manufacturing and quality-control processes.
Prepare a formulation to combine two active ingredients into one tablet. When you formulate two actives into one tablet you need to take into account the physical nature of each active (and other excipients included in the formulation), and how the active ingredients will behave when combined in the formulation.
A wide range of excipients can be used, such as fillers, binders, disintegrants, lubricants, glidants and other formulation ingredients approved for use. The finished excipient system must be capable of yielding a tablet with sufficient strength, without making the tablet unduly large.
Assessment of compatibility may be carried out during formulation development to measure the interaction of both APIs and the excipients chosen. This forms the foundation for making an intact, manufacturable formulation.
Since the tablet contains 700 mg of combined active ingredients, effective powder handling is an important consideration for development. The formulation must flow well into the tablet compression machine while also achieving good powder flow and blend uniformity.
The formulation may be designed by direct compression or a granulation approach, which can be advantageous if better flowability, density and compressibility are needed.
Track particle-size distribution, moisture content, bulk density and flow properties during development. Processing parameters should be such as to prevent segregating of the material and allow uniform feeding into the tablet press.
The tablet is moved through the compression stage where the blend or granules are compressed to form the finished product. As there is a high active content in the formulation the compression conditions must be optimized to attain appropriate tablet hardness and size.
This lists a few possible influencing factors such as pressure, feeder settings, turret speed, punch pattern and dwell time. These can affect hardness, thickness, friability and appearance. In-process checks may be performed to monitor weight and physical characteristics of a batch.
Here too, it is desirable to prevent common manufacturing faults, such as caping, lamination, sticking or tablet weight variation. A tight compression window preserves reproducibility in routine production.
Dissolution testing is a key way of characterising the release of the APIs from the combination tablet under specified in vitro conditions. As the combination tablet contains two APIs, they can be assessed separately by an appropriate analytical method.
Dissolution may be affected by any of the formulation variables such as the level of binder, type of disintegrant, structure of the granules, compression pressure and tablet porosity. Comparison of development batches could thus be made to determine appropriate processing conditions.
The finished-product evaluation can consist of identification of, assay of either component, content uniformity, dissolution, disintegration, related substances, hardness, friability and other relevant tests.
Two active ingredients (Ofloxacin & Ornidazole) can be seperated by an analytical method and both active compounds should be determined with the sample matrix. Methodology used for different compounds seperation will be appropriate.
Additional quality-control tests might include analysis of degradation by-products and other chemical tests. Test validation or qualification will determine the appropriate sensitivity, accuracy, precision and specificity for a proposed test method.
Representative sampling from the manufacturing batch is essential, because the final result will be representative of the tablets' overall uniformity. For this reason, full batch records ensure traceability from raw materials to finished-product release.
Stability testing can be used to determine if a formulation of Ofloxacin 200MG + Ornidazole 500MG Tablets, retains the specified quality at designated storage conditions within specified storage period. Assay, related substances, dissolution, appearance, moisture, hardness, packing etc. may be tested depending upon the specification of product.
Select packaging system based on the observed stability profile of the formulation. For protection from environment and compatibility of the tablets, strips, blister packs or appropriate containers can be studied.
This dual-active tablet may be used as one part of a multi-product PCD Pharma Franchise range for pharma companies with the extensive portfolio of Pharma Franchise Products, backed by controlled formulation development, analytical testing, stability studies, and suitable packaging.
The manufacturing journey from API compatibility, high-load powder processing, compression, two component dissolution testing, analytical verification, stability testing and monitoring to final packaging, has been directed by the unique properties of this combination. These product-specific controls help ensure that the Ofloxacin 200MG + Ornidazole 500MG Tablets are of consistently high quality.
Ofloxacin 200MG + Ornidazole 500MG Tablets formulation, dual-API manufacturing, quality testing, stability and packaging details for pharma products.