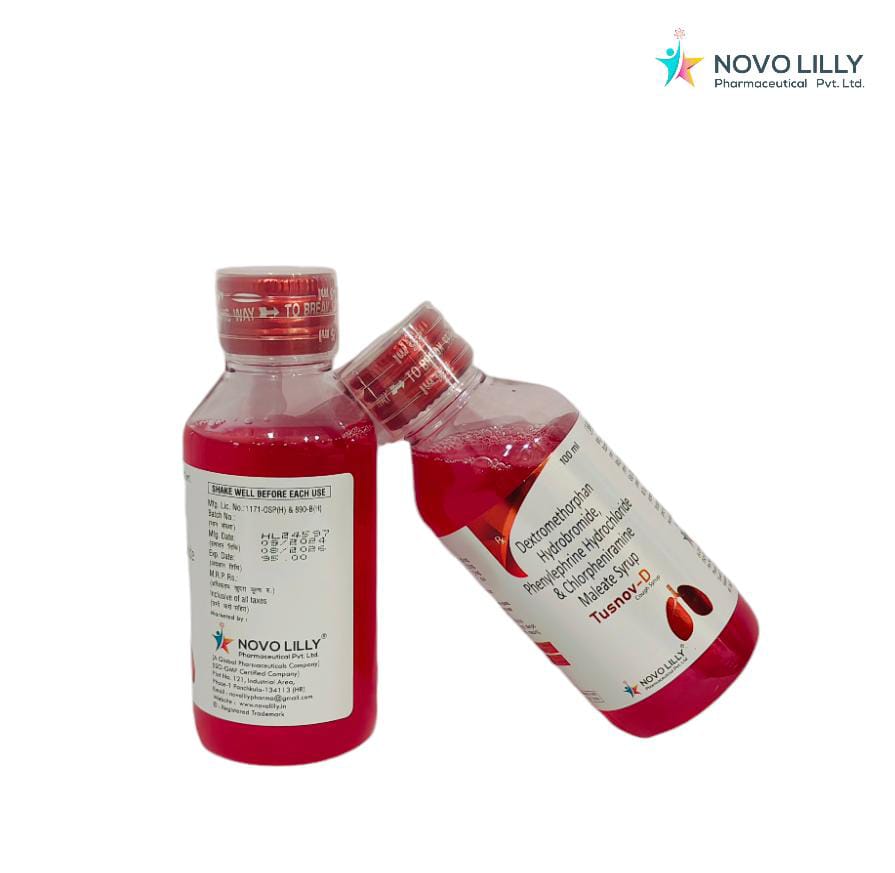
Dextromethorphan 10 MG + Chlorpheniramine Maleate 2 MG + Phenylephrine Hydrochloride 5MG Syrup is a multi-component oral liquid medicine which comprises three active pharmaceutical elements presented in an identical syrup base. Like all the preparations, this multi preperation syrup has to result in a compatible mixture of Ingredients, suitable accuracy in composition, uniformity of liquid phrase & viscosity, low pH and proper packaging & presentation. For pcd pharma franchise, pharma companies can manufacture combination & multi drug syrups.
The formulation has Dextromethorphan 10 MG, Chlorpheniramine Maleate 2 MG and Phenylephrine Hydrochloride 5MG as per composition provided. Due to three actives being put in a common liquid phase, the manufacturing process has to be set to ensure that the ingredients are well dispersed in the final bulk.
The syrup base can include the blend of approved pharmaceutical grade excipients used in accordance with the approved formulation. They may include ingredients to provide the necessary solubilisation, viscosity, sweetness, flavour and preservation and physical stability. The precise choice of excipients should be in line with the completed product specification and formulation needs.
Multi-active syrup formulation parameters The critical factors for formulation are the ability to uniformly disperse each of the ingredients into the liquid system. The physicochemical properties of Dextromethorphan, Chlorpheniramine Maleate and Phenylephrine Hydrochloride are considered as part of the formulation development to identify the required processing conditions and excipients.
The lower level of chlorpheniramine maleate is also sensitive to weighing and mixing. Controlled addition and mixing ensure a smaller amount of variation in concentration within the vessel. The remaining active ingredients are then added sequentially using the validated manufacturing sequence defined for the product.
Ingredient order and water quality are also factors which can affect the finished formulation. Materials can be pre-dispersed or pre-mixed before entering the main batch, depending on the formulation of the finished product. Good agitation will produce a uniform liquid system and should not incorporate undue amounts of air.
During manufacturing, controls for mixing time, temperature, pH and batch size can be maintained to acceptable specifications. These control controls help to ensure reproducibility between batches of manufacture.
The physical attributes of the finished product are significantly impacted by the syrup vehicle. Using a liquid medium that is sufficiently liquid gives the product the consistency it needs and allows for even mixing of the active components. The viscosity should stay within the range specified to allow for proper filling and stable product in storage.
Depending on the approved formulation, flavouring and sweetening agents may also be added to achieve the desired organoleptic characteristics. The effect of these agents on the composition in conjunction with the active substances and other excipients should be considered. Overprocessing or inappropriate mixing of ingredients can change the visual appearance, taste or the physical structure of the syrup.
PH is another quality indicator for liquid formulations. Specific pH values can play a role in the stability of the formulation as well as overall compatibility with chosen excipients and packaging components. As such, the finished product may be tested for pH and viscosity as part of in-process and finished-product specifications.
Visual inspection is applicable to clarities, colours, consistency, the presence of foreign matter, etc. The appearance should be consistent with the approved product specification.
Manufacturing of the syrup Preparation and confirmation of the raw materials required for production are done at this stage. The individual component and excipient used are weighed following the approved formula of the batch. The ingredients are finally processed by following the manufacturing process as described.
The liquid vehicle is formulated in the liquid vehicle Manufacturing area, with Pharmaceutical Grade Water and other approved excipients. Active ingredients are added to the vehicle according to a predetermined mixing procedure for homogeneity. The batch is then subjected to volume adjustments, pH adjustments (when required), filtration or other appropriate processing.
Quality control testing offers a critical validation step. Tests may be conducted to determine the identity and assay of the individual active ingredients, the pH, viscosity, appearance, fill volume, microbial quality, and other specified characteristics as defined by the approved specification.
As formulation contains three active substances analytical methods should have sufficient specificity and accuracy for each of these. Sampling should be representative of the whole batch so that the final test results are indicative of the finished product.
Batch Traceability Documention Manufacturing documentation is similarly useful for batch traceability. The records for all raw material, equipment cleaning, processing parameters, in-process observations, laboratory testing and final packaging can be stored within the controlled manufacturing system.
Bottle/Closure System The packaging material selection, particularly the bottles and closures has a significant impact on many facets of development of Dextromethorphan 10 MG + Chlorpheniramine Maleate 2 MG + Phenylephrine Hydrochloride 5MG Syrup. The bottle/closure combination used should offer suitable protection from environmental factors yet be compatible with the product in the specified storage conditions.
Typical systems for packaging pharmaceutical syrup include suitable bottles of plastics or glass equipped with appropriate closures. For the ultimate pack system, considerations should be given to leakage, closure integrity, fill-volume uniformity, handling and compatibility of the pack with the liquid formulation.
By conducting a stability assessment, quality parameters including, appearance, colour, pH, viscosity, assay of active ingredient, microbiological standards and the integrity of the packaging can be checked over the scheduled storage time. This can be used to determine if the product will retain the qualities demanded when stored at this temperature.
In fact, the standardized formulation of PCD Pharma Franchise in Syrup can be applied to a variety of medicinal products through a wide range of specifications, packaging, batch documentation, and Quality Control Protocols. Product development must be done in accordance with the demonstration content, and pharmaceutical quality standards, 23.
Thus the dependability of multi-active syrup directly results from the integrated control of raw materials, liquid phase processing, uniformity of ingredients, viscosity, pH, analytical assessment, suitable packaging considerations and stability considerations to give a professional manufactured pharmaceutical liquid dosage form.
Dextromethorphan, Chlorpheniramine Maleate & Phenylephrine Hydrochloride syrup with focus on formulation, manufacturing, quality and stability.