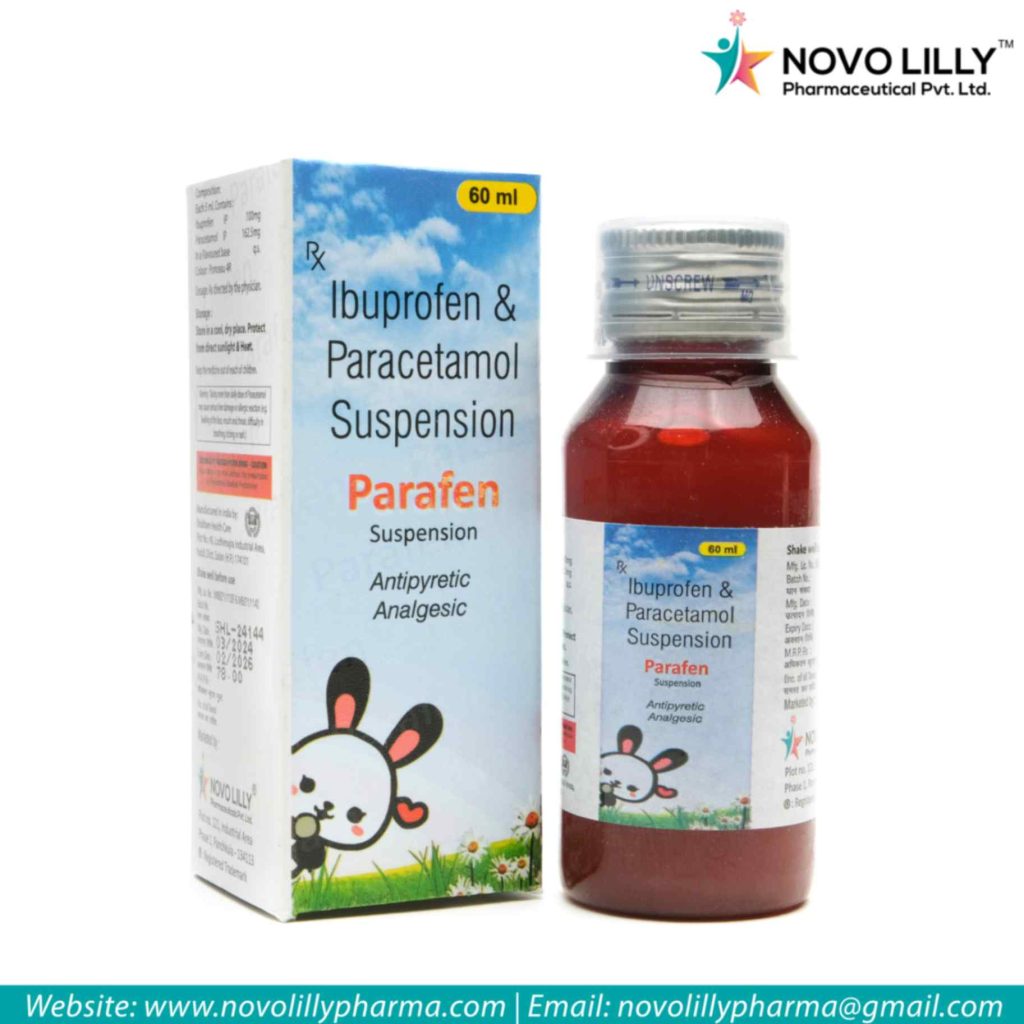
Join us at the platform of publishing the information regarding the Ibuprofen 100MG + Paracetamol IP 162.56MG Suspension, that is a strong oral liquid formulation. Description of formulation: What are the ingredients in this suspension? The suspension consists of a perfect mixture of two ingredients called as paracetamol and the name of the second ingredient. If you are a pharma company and wish to include this into the oral-liquid formulation range of your PCD Pharma Franchise, then PCD Pharma Franchise manufacturing and quality system will be on offer.
The process begins by analyzing the physical characteristics of each active pharmaceutical ingredient. How do you equalize powder materials with different particle features and solubility profiles? Creating the right liquid vehicle to complement all ingredients is how you achieve this.
The inclusion of appropriate wetting agents, suspending agents, viscosity modifiers, sweetening agents, flavoring agents, preservative and other permitted excipients must be considered. Whatever substance that has been chosen must be in accordance with the final formula for proper compatibility.
The steps of the manufacturing process should ensure even distribution of ibuprofen and paracetamol through the bulk. The sequence is planned according to the properties of the raw materials and the suspension system.
To avoid lumping or quick settling it's necessary to properly wet and disperse ibuprofen and other particles in suspension. Particle size has an impact on sedimentation, viscosity, color, and redispersion.
Informulation development the active ingredients are pre-dispersed before added to the primary vehicle. A controlled agitation is used to disperse the particles in formation without putting excess air into the formulation.
The bulk suspension is tested at different manufacturing stages to verify uniformity. Mixing time, speed, temperature, hold time are controlled within the limits of the process.
Viscosity: Sedimentation, pourability, fill accuracy, and redispersibility are all significantly affected by an oral suspension. The formulation should have a designed rheological profile that leads to physical stability and easy dispensing.
Dose-volume uniformity depends on the homogeneity of the suspension prior to filling as well as during normal processing. Also important are the shape of the bottle and the style of closure.
Physical Testing viscosity, pH, appearance, colour, sedimentation characteristics, particle size distribution and redispersibility These properties are examined during development and stability studies to formulate exact specifications.
How do you mask the taste of a number of actives? The flavor and sweetener base has to be compatible. Flavour must be well matched to the vehicle, and, once in use, must remain consistent.
Manufacturing liquids entails the formulators utilization of the vehicle, the active components and the auxiliary excipients in a controlled process. This process is meant to achieve uniform distribution of ingredients and prevent or limit introduction of air or foaming.
Before filling, the completed bulk product undergoes in-process testing. During filling, fill-volume control and container examination ensure uniformity from batch to batch.
This quality-control testing covers the individual active substances of the Ibuprofen 100MG + Paracetamol IP 162.56MG Suspension. As a general rule, testing of the individual active substances may consist of identification, assay, pH, viscosity, microbial quality, fill volume, redispersibility and so on according to specifications.
Having two active ingredients in the same liquid matrix, the analytical method should have some selectivity so that the individual components can be accurately quantified. Validation or qualification can be used to support routine quality assessment.
Stability studies also monitor the assay, related substances, pH, viscosity, appearance, sedimentation and redispersibility and microbial quality, and the state of the container. They verify that the suspension is stable and provides its described performance till the end of its shelf life.
The type of packaging is determined according to the physical and stability properties of the suspension. Pharmaceutical Grade bottles, along with their closures are tested for breakage, leakage, container-closure integrity and emptying.
The bottle design should be such as to allow ease of handling, yet safeguard the liquid in transit and storage. Labels should declare composition, strength, batch data, manufacturing data, shelf life, storage data and other related information.
This combination active suspension is best suited for a structured oral-liquid range by PCD Pharma Franchise for Pharmaceutical companies. This PCD Pharma Franchise for Pharma Franchise companies have a standardized set of raw-material specifications, regulated manufacturing processes, analytical testing, stability testing, and packaging.
Product consistency becomes central from active-ingredient characterization, particle wetting to rheology control, flavor optimization, bulk uniformity testing, analytics verification, stability studies, and finally filling. A formulation-specific approach is key to ensuring your product IBUPROFEN 100MG + PARACETAMOL IP 162.56MG Suspension stays consistent within the defined profile over its shelf life.
Ibuprofen 100MG + Paracetamol IP 162.56MG Suspension formulation, liquid manufacturing, quality control, stability and packaging details.