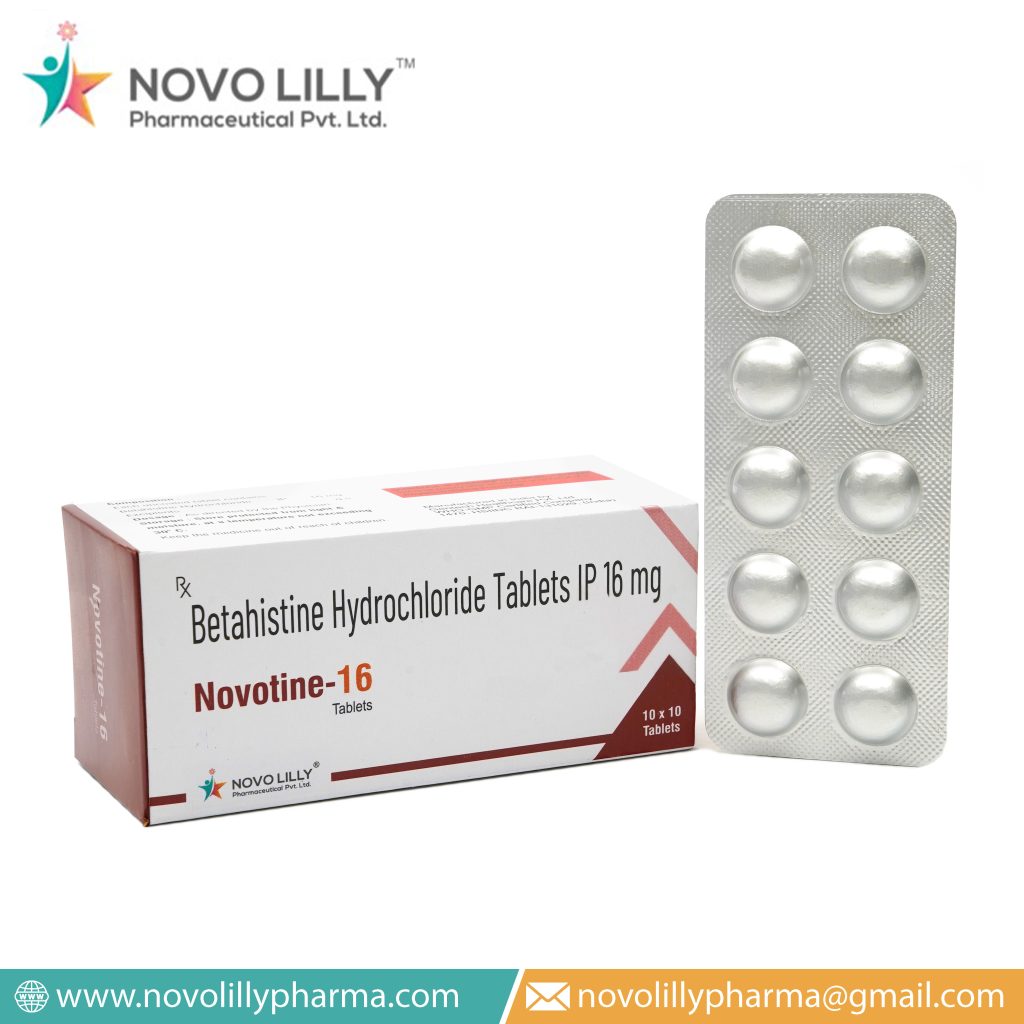
Betahistine 16MG Tablets Betahistine 16MG Tablets are solid oral dosage form in which specific amount of betahistine is present per tablet. The product development of this drug involves selection of effective-ingredient uniformity, compatible excipients, and powder stability and good compressibility along with stability of the final dosage form. For Pharma franchise holders aiming to scale up their portfolio, betahistine 16 MG tablets can be used as part of a Pharma franchise PCD range.
The formulation of Betahistine 16MG Tablets begins with the careful characterization of the active pharmaceutical ingredient and any excipients chosen. Particle size, bulk density, flowability, moisture content and compatibility can all affect how the tablets will perform.
The composition may include appropriate diluents, binders, disintegrants, lubricants, glidants, and other excipients permitted in the final formulation. To ensure the active ingredient is evenly dispersed throughout the batch, the blending method is optimized to maintain proper content uniformity.
Where differences in particle size or density of various components in the formulation is apparent then the manufacturing process can adopt corresponding sieving, pre-blending or granulation steps to produce a more uniform powder or granule prior to compression.
The physical properties of the formulation blend can influence how tablets are made. Tablets which flow well will produce a relatively uniform quantity of material transfer into the tablet compression machine and help produce tablets of constant weight.
The blend of powders is then either directly compressed, or formed using a granulation technique, with the exact technique utilized based on the powders flowability and compressibility, which is contingent on the moisture sensitivity, and the performance specifications decided in the development process.
Can the physical quality of the disintegrating tablets be influenced? Yes, with compression force, turret speed, feeder operation and tooling arrangement can affect hardness, thickness, friability and disintegration. These parameters are thus maintained within defined limits during production.
The physical quality of Betahistines 16MG Tablets can be checked by established in-process and finished-product specifications. The appearance of tablets, dimensions, variation in weight, friability, hardness and disintegration are observed as per the relevant product specification.
Consistent tablet surface and dimensions are essential to provide consistent packaging and presentation. The level of compression can influence disintegration behaviour of the tablet and may influence handling properties during subsequent processing if it is too light.
For a coating system in the formulation, more controls can be added to the coating weight gain, colour uniformity, surface finish, and manufacturing process. The finished dosage form should be stable and uniform throughout the storage time.
Quality Control (QC) of the Betahistine 16MG Tablets Active ingredient and relevant finished-product quality attributes are used as quality assurance measures, depending on the specification of active ingredient and finished-product. Analytical control assays can vary according to the lot release specification of the drugs, such as identification, assay, content uniformity, disintegration, related substances, moisture, and other tests.
In-process testing to uncover manufacturing variation early Samples can be collected at various points during compression to determine weight and other attributes.
Analytical procedures should be suitably validated or qualified for their intended use. Adequate sampling and appropriate handling and testing of samples are especially relevant to establish comparability between batches of products.
Stability testing decides if Betahistine 16MG Tablets possess the defined physical and chemical characteristics for the full duration of the shelf life. The stability of the product may be observed using such tests as appearance, assay, dissolution, related substances, and moisture.
Packaging considerations will be dictated by the product's established stability profile, which would include consideration of the product's environmental sensitivities. Blister packs/strips, or appropriate container systems may be considered depending on the product and market.
The packaging system shall allow sufficient safeguard for transport, storage and routine handling. Maintaining the quality of the tablets by sealing and matching of packaging materials shall also ensure correct identification and traceability of batch.
Betahistine 16MG Tablets A systematic approach to managing the flow of active-ingredient treatment, product powder, compression stresses, analytical examination and packing. Controlled manufacturing process Regular-sized lot production ensures the same quality for all tablets.
This type of formula can be launched in a structured catalogue of tablets with a branded PCD Pharma Franchise for diversified franchise prospects and specifications for raw materials, manufacturing, quality evaluation, and stability testing.
From upfront material qualification and blend formulation through compression, analytical verification, stability testing and assessment, and final packaging, each step is essential to ensuring consistent Betahistine 16MG Tablets. An organized approach to product development offers assurance when producing product and helps preserve the quality of the finished dosage form for its forecasted shelf life.
Betahistine 16MG Tablets with formulation, manufacturing, quality control, stability and packaging details for pharmaceutical product development.