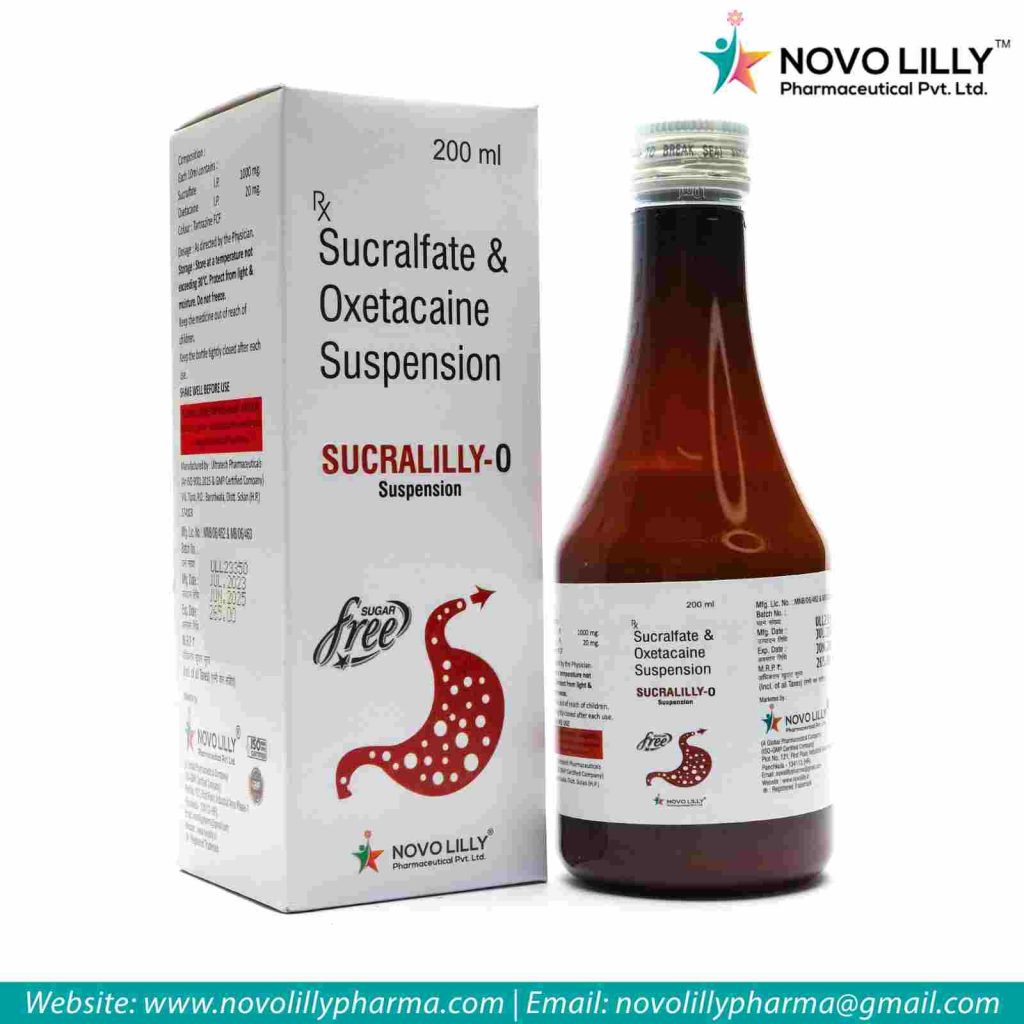
SUCRALFATE 1000 MG & OXETACAINE 20 MG SUSPENSION is a dual-component oral liquid formulation containing sucralfate and oxetacaine in a controlled suspension vehicle. The formulation combines a comparatively high quantity of sucralfate with a lower-strength oxetacaine component, making uniform distribution an important part of product development. Since sucralfate is handled as a dispersed material, the formulation requires careful attention to wetting, particle size, viscosity, sedimentation, redispersibility, and dose consistency. For pharmaceutical manufacturers developing a diversified PCD Pharma Franchise portfolio, controlled suspension technology is important for achieving reproducible batch quality.
The formulation contains two active ingredients with different concentration levels and physical characteristics. Sucralfate forms the major dispersed component, while oxetacaine is incorporated at a substantially lower concentration. This difference creates an important formulation challenge because the two ingredients must remain uniformly distributed throughout the finished bulk.
The vehicle may contain purified water, suspending agents, wetting agents, viscosity modifiers, sweetening materials, flavouring components, preservatives where appropriate, and other pharmaceutical excipients. The exact excipient combination depends on the desired physical characteristics and development strategy.
During formulation development, the compatibility of sucralfate and oxetacaine with the selected vehicle is assessed. Particle size, density, moisture, solubility behaviour, and rheology are considered while establishing the final suspension architecture.
Efficient wetting of sucralfate is a key manufacturing step because poorly wetted particles can form agglomerates or remain unevenly distributed within the liquid. A controlled wetting phase may therefore be prepared before the active material is incorporated into the main vehicle.
Oxetacaine requires separate consideration because of its lower concentration within the formulation. A suitable premix or controlled dilution approach may be used during development to promote its uniform incorporation into the larger suspension volume.
The order of addition can significantly influence the final product. Suspending agents may be hydrated separately, followed by controlled incorporation of the active phase under defined agitation conditions. Mixing speed, time, temperature, and homogenization parameters are established through formulation development and scale-up studies.
A successful suspension should maintain suitable physical stability without becoming excessively viscous. Rheological behaviour influences particle settling, pourability, filling performance, and ease of redispersion.
Because sucralfate is present at a relatively high level, sedimentation behaviour needs particular attention. Particle-size distribution and the selected suspending system can influence whether the settled material forms a loose sediment that can be readily redispersed or a compact layer that is more difficult to redisperse.
Redispersibility testing can be performed at defined stages of stability evaluation. Viscosity measurements, sedimentation volume, visual appearance, and homogeneity provide additional information about the physical performance of the formulation.
The finished suspension should maintain consistent characteristics after appropriate controlled shaking, allowing the bulk product to remain representative of the approved formulation.
Manufacturing begins with qualification and verification of all active ingredients and excipients. Accurate weighing is particularly important because sucralfate and oxetacaine are present at substantially different concentrations.
In-process testing can include appearance, pH, viscosity, bulk homogeneity, temperature, and other critical process parameters. The mixing sequence and duration are controlled to maintain reproducibility between batches.
Finished-product analysis may include identification and assay of both active ingredients, pH, viscosity, microbial quality, fill volume, sedimentation behaviour, and redispersibility. Analytical procedures should be capable of accurately evaluating the two components independently.
Sampling must also be representative of the batch because suspended formulations can exhibit concentration differences if the bulk is not adequately maintained in a homogeneous state during filling.
Stability studies for SUCRALFATE 1000 MG & OXETACAINE 20 MG SUSPENSION can evaluate changes in assay, pH, viscosity, appearance, sedimentation, redispersibility, microbial quality, and other relevant attributes over the proposed shelf life.
Packaging compatibility is particularly important for a liquid suspension because the container should protect the formulation while allowing practical dispensing. Pharmaceutical-grade plastic or glass bottles may be evaluated according to the formulation's compatibility and stability requirements.
The closure system should minimize leakage and external contamination while maintaining product integrity. Fill-volume accuracy, cap torque or closure performance, container interaction, and physical protection during transportation can also be assessed.
Stability studies may additionally consider temperature and light exposure according to the formulation-development protocol.
The final product can be presented in a suitable bottle-and-closure configuration selected according to the suspension's physical and stability requirements. Consistent filling, secure sealing, accurate batch coding, and appropriate labeling support traceability across the pharmaceutical supply chain.
For pharmaceutical businesses, SUCRALFATE 1000 MG & OXETACAINE 20 MG SUSPENSION can be included within a broader PCD Pharma Franchise product portfolio when supported by appropriate regulatory requirements and standardized quality specifications. Reliable active dispersion, controlled viscosity, reproducible dispersibility, analytical verification, and compatible packaging provide the technical foundation for consistent manufacturing and organized pharmaceutical distribution.
Sucralfate 1000mg + Oxetacaine 20mg Suspension with formulation, manufacturing, quality control, stability and packaging details.